

Activated Alumina
Why Choose Us?
Rich Experience
PM has been established for more than 20 years, is a leading manufacturer specializing in tower packing we have been focusing on building an one-stop chemical packing E-commerce platform, aiming at satisfying customers comprehensive chemical packing demand and providing fast full service.
Global Sales Network
The products are exported to the North America, South America, Europe, Southeast Asia/ Mideast, Africa, East Asia (Japan/ South Korea). more than 120 countries.
Quality Service
We not only promote qualified product, also emphasize on providing professional technique and good service. Providing fast and convenient delivery of goods for customers is our constant pursuit. In order to meet customers need for products & services anytime and anywhere, we have established a strong service system.
Advanced Equipment
75 Meters full automatic production line, Packaging Machine, Sintering Furnace,Forming Machine,Vacuum Extraction Machine,Mixing and Stir Powder Tower, Carbon Dioxide Tester,Resistance Furnace, Drying Cabinet,Digital Display Comprehensive Testing Instrument for Strength of Engineering Ceramics, Particle Abrasion Tester, Moisture Tester, Particle Strength Tester, Digital Viscometer,Electrical Scale.
Activated alumina is manufactured from aluminium hydroxide by dehydroxylating it in a way that produces a highly porous material; this material can have a surface area significantly over 200 m2/g. The compound is used as a desiccant (to keep things dry by adsorbing water from the air) and as a filter of fluoride, arsenic and selenium in drinking water. It is made of aluminium oxide (alumina; Al2O3). It has a very high surface-area-to-weight ratio, due to the many "tunnel like" pores that it has. Activated alumina in its phase composition can be represented only by metastable forms (gamma-Al2O3 etc.).


Benefits of Activated Alumina
High Adsorption Capacity
Activated alumina desiccant has impressive adsorption capacity due to its large surface area and pore structure. This makes it highly efficient in the removal of contaminants, ensuring clean and purified liquids or gases.
Thermal Stability
Activated alumina exhibits excellent thermal stability, allowing it to withstand high temperatures without degrading or losing its adsorption properties. This feature makes it suitable for applications that involve elevated temperatures.
Regenerability
One of the key advantages of activated alumina is its regenerability. After reaching its adsorption capacity, it can be easily regenerated and reused, reducing operational costs and environmental impact.
Versatility
Activated alumina's versatility stems from its wide range of applications. Its adaptability to different environments and ability to target specific contaminants make it an invaluable asset across various industries.
Activated Alumina Applications
Activated alumina is used for a wide range of adsorbent and catalyst applications including the adsorption of catalysts in polyethylene production, in hydrogen peroxide production, as a selective adsorbent for many chemicals including arsenic, fluoride, in sulfur removal from fluid streams.
Desiccant
Used as a desiccant, it works by a process called adsorption. The water in the air actually sticks to the alumina itself in between the tiny passages as the air passes through them. The water molecules become trapped so that the air is dried out as it passes through the filter. This process is reversible. If the alumina desiccant is heated to ~200 °C, it will release the trapped water. This process is called regenerating the desiccant.
Fluoride Adsorbent
Activated alumina is also widely used to remove fluoride from drinking water.
Activated alumina filters can easily reduce fluoride levels from 10 ppm to less than 1 ppm. The amount of fluoride leached from the water being filtered depends on how long the water is actually touching the alumina filter media. Basically, the more alumina in the filter, the less fluoride will be in the final, filtered water. Lower temperature water, and lower pH water (acidic water) are filtered more effectively too. Ideal pH for treatment is 5.5, which allows for up to a 95% removal rate.
Vacuum Systems
In high vacuum applications, activated alumina is used as a charge material in fore-line traps to prevent oil generated by rotary vane pumps from back streaming into the system. A baffle of activated alumina can also replace the refrigerated trap often required for diffusion pumps, though this is rarely used.
Biomaterial
Its mechanical properties and non-reactivity in the biological environment allow it to be a suitable material used to cover surfaces in friction in body prostheses.
Defluoridation
Defluoridation is the downward adjustment of the level of fluoride in drinking water. Activated Alumina process is one of the widely used adsorption methods for the defluoridation of drinking water.
How To Make Activated Alumina
The process described below for making activated alumina desiccant is intended for informational purposes only and may not be complete.
Raw Material Preparation
The raw material used in the production of activated alumina is typically aluminum hydroxide. The aluminum hydroxide is processed to remove impurities and then ground into a fine powder.
Activation
Activation involves subjecting the powder to temperatures nearing 1000°C. This high-temperature treatment causes the aluminum hydroxide to undergo a phase change and transform into gamma alumina, which has a larger surface area and greater porosity.
Impregnation
After activation, the gamma alumina is impregnated with a chemical solution that enhances its moisture-adsorbing properties. Common impregnating agents include phosphoric acid, potassium permanganate, and sodium hydroxide. The choice of impregnating agent depends on the specific application of the activated alumina.
Drying and Packaging
The final step in the manufacturing process is drying and packaging the activated alumina desiccant. The impregnated gamma alumina is typically dried in a rotary kiln to remove any residual moisture. The dried activated alumina is then packed in bags or drums and shipped to customers.
While they often perform the same process of adsorbing moisture, activated alumina and molecular sieve differ in many ways. Molecular sieve features pores whose size can be adjusted by ion exchange, allowing them to separate molecules based on size discrimination, a task other adsorbents are not capable of. This is why, for example, molecular sieve is used in the separation of ethanol and water.
The sizes of the pores of activated alumina cannot be tailored and are not necessarily uniform. However, activated alumina has its own pros. Activated alumina shows a higher affinity for water than molecular sieve, so it is often used in the drying of various gas and liquid streams, instances when it is important to adsorb the most moisture possible. Its high crush strength allows activated alumina to withstand the high pressures of industrial applications.

Features of Activated Alumina
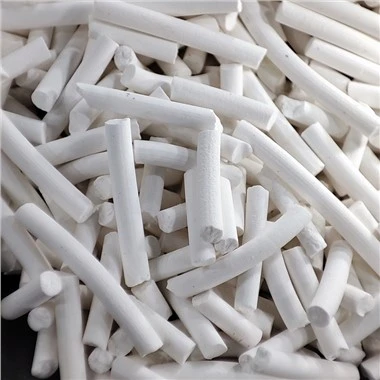
Activated alumina is aluminum oxide in the form of very porous spheres that are literally "tunneled" at the microscopic level. This makes them handy for a number of different jobs. For example, they can be used to dry gases. The drying of gases is often vitally necessary for safe transportation of volatile gases. Gases such as propane must be dried before use to prevent corrosion of equipment that could result in dangerous leaks.
Activated alumina adsorbs, not absorbs. There is an important difference. For example, a sponge will absorb water, but the water molecules do not actually bond with those of the sponge. And so, the water can simply leak out or evaporate after a while. Activated alumina adsorbs. When a chemical is drawn into the pores of an activated alumina sphere, it actually bonds with the solid material. Once in, it won't come out without considerable heating.
Activated Alumina's Top 5 Superpowers
Fluoride Fighter: Bye-bye, excess fluoride! Activated alumina takes charge, ensuring your water is free from too much of this dental superhero.
Arsenic Avenger: The porous structure of activated alumina? It's like a fortress against arsenic, which could be lurking in your water.
Chlorine Champion: Tired of that strong chlorine smell? Activated alumina is here to tone down the party and give you a gentler shower experience.
VOC Vanquisher: Volatile Organic Compounds (VOCs) beware! Activated alumina's got your number and is ready to give you the boot.
Heavy Metal Hero: Lead, copper, and iron? No match for activated alumina. It's like the superhero dream team for purer, safer water.
How Does Activated Alumina Help in an Air Dryer
Activated alumina has a highly porous surface which offers a large surface area to which moisture molecules adhere, as it is an excellent adsorbent material. Activated alumina aids in the drying process in an air dryer by adsorption of compressed air. Adsorption is the process by which molecules of the mixture adhere to a particular surface, but don't get absorbed into the material. This way the activated alumina can adsorb the moisture molecules and remove any vapor/gas/humidity from the air of your air dryer.
Activated alumina is a very effective desiccant, and is also chemically inert, and reusable in nature, making it a great sustainable choice for your compressed air dryer. Its efficiency is highly durable, and since it is non-toxic in nature, it is safe to use even in a home setting.
When water vapor or gas comes into contact with a bed of alumina beads that have been activated, the pores in the desiccant dryer alumina beads allow the numerous water vapor molecules to be adsorbed and trapped in the alumina beads material. This adsorption process reduces the compressed air's dew point levels, so it won't condense onto the material but instead, you'll get a dry product.
Alumina activated beads have a high ability to adsorb moisture due to its hygroscopic substances, which makes a desiccant dryer a great option for applications where you need to keep the humidity/moisture levels low, like here in the case of an air dryer. It is also capable of absorbing moisture levels down to -50°F dew point or even lower in some cases, depending on how the compressed air dryer system is designed and how it works.
Activated alumina balls/desiccant dryers have a lot of benefits, but one of the most important one is that they can last for a long time at different varying temperatures. It's not affected by high temperatures, so it's the perfect choice of desiccant for industrial applications where you might be using compressed air or gas, like in air dryer systems.
Alumina activated balls can be used in a variety of industries due to their high compatibility capabilities with a variety of gases, compressed air, and chemicals, in general, with the adsorption and purification of various gases and liquids. This is a great advantage for various industries to use alumina desiccant for all their air drying needs.
The process of adsorption requires the generation of dust, and activated alumina beads are designed and can greatly help to reduce the amount of dust produced during this process. It also helps minimize the contamination of sensitive applications and helps with the maintenance.
Unlocking the Potential of Activated Alumina
Cost-Effectiveness
One of the key benefits of activated alumina is its cost-effectiveness, as it can be regenerated and reused multiple
Times without losing its efficiency. This ability to regenerate and reuse activated alumina makes it a more economical choice compared to other adsorbents and desiccants, reducing overall operating costs in various applications.
Environmental Benefits
Activated alumina offers significant environmental benefits due to its effectiveness in removing harmful contaminants from water and air. By using activated alumina to treat water, industries can help reduce the presence of toxic substances and protect both human health and the environment. Moreover, the use of activated alumina in air purification systems helps to maintain clean air and reduce pollution, contributing to a healthier living and working environment.
Enhancing Product Quality
In industries like petrochemicals and pharmaceuticals, the presence of moisture or contaminants can have a detrimental impact on product quality. Activated alumina's superior desiccant and adsorbent properties make it an essential tool in these industries, ensuring that products meet the highest quality standards and have a longer shelf life.
Our Factory
Super Packing Mall is a leading manufacturer specializing in tower packing. Our tower packing is well accepted by overseas customers. It includes metal, ceramic, plastic random packing, structured packing, ceramic ball, water treatment material, adsorbent etc.
Our Product are used for industries like chemical industry, chemical fertilizer industry, oil refining, petrochemical industry and natural gas, fine chemical, flavors factory, air pollution control, isomer separation, the separation of thermally sensitive materials etc.